Galvanic Series Chart: Metal Compatibility Table (Free PDF)
Galvanic series in seawater with potentials vs SCE, anodic index limits, fastener compatibility matrix and corrosion fixes. Free PDF, PNG and CSV downloads.
Galvanic Series in Flowing Seawater, Corrosion Potentials vs SCE (MIL-STD-889 / ASTM G82 derived)

| Rank | Metal or alloy | Condition | Corrosion potential (V vs SCE) | Position in a couple |
|---|---|---|---|---|
| 1 | Magnesium and magnesium alloys | - | -1.60 to -1.63 | Most anodic, sacrificial |
| 2 | Zinc, zinc plating, hot-dip galvanizing | - | -0.98 to -1.03 | Anodic, sacrificial |
| 3 | Aluminum alloys (1100, 3003, 5052, 6061, 7075) | - | -0.76 to -1.00 | Anodic |
| 4 | Cadmium plating | - | -0.66 to -0.71 | Anodic |
| 5 | Mild steel, wrought iron | Clean, bare | -0.60 to -0.71 | Anodic |
| 6 | Cast iron | - | -0.60 to -0.71 | Anodic |
| 7 | Low-alloy (HSLA) steel | - | -0.56 to -0.64 | Anodic |
| 8 | Stainless steel 410, 416 | Active | -0.46 to -0.58 | Anodic when active |
| 9 | Stainless steel 302, 304, 321, 347 | Active | -0.46 to -0.57 | Anodic when active |
| 10 | Stainless steel 430 | Active | -0.45 to -0.57 | Anodic when active |
| 11 | Nickel-chromium alloy 600 (Inconel 600) | Active | -0.35 to -0.48 | Anodic when active |
| 12 | Stainless steel 316, 317 | Active | -0.35 to -0.46 | Anodic when active |
| 13 | Aluminum bronze (92% Cu, 8% Al) | - | -0.31 to -0.42 | Mid series |
| 14 | Copper | - | -0.30 to -0.57 | Mid series |
| 15 | Tin | - | -0.31 to -0.34 | Mid series |
| 16 | Naval brass, yellow brass, red brass, Muntz metal | - | -0.30 to -0.40 | Mid series |
| 17 | Lead-tin solder (50/50) | - | -0.29 to -0.37 | Mid series |
| 18 | Admiralty brass, aluminum brass | - | -0.28 to -0.36 | Mid series |
| 19 | Manganese bronze | - | -0.27 to -0.34 | Mid series |
| 20 | Silicon bronze (96% Cu) | - | -0.26 to -0.29 | Mid series |
| 21 | Stainless steel 430 | Passive | -0.20 to -0.30 | Mid series |
| 22 | 90-10 copper-nickel | - | -0.21 to -0.28 | Mid series |
| 23 | 80-20 copper-nickel | - | -0.19 to -0.24 | Mid series |
| 24 | Lead | - | -0.19 to -0.25 | Mid series |
| 25 | 70-30 copper-nickel | - | -0.18 to -0.23 | Mid series |
| 26 | Nickel-aluminum bronze | - | -0.14 to -0.22 | Mid series |
| 27 | Nickel 200 | - | -0.09 to -0.20 | Cathodic, protected |
| 28 | Silver | - | -0.09 to -0.15 | Cathodic, protected |
| 29 | Nickel-chromium alloy 600 (Inconel 600) | Passive | -0.09 to -0.15 | Cathodic, protected |
| 30 | Nickel-copper alloys 400, K-500 (Monel) | Passive | -0.02 to -0.13 | Cathodic, protected |
| 31 | Stainless steel 302, 304, 321, 347 | Passive | -0.05 to -0.13 | Cathodic, protected |
| 32 | Stainless steel 316, 317 | Passive | 0.00 to -0.10 | Cathodic, protected |
| 33 | Titanium | Passive | -0.05 to +0.06 | Cathodic, noble |
| 34 | Gold | - | +0.07 to +0.20 | Most cathodic, noble |
| 35 | Platinum | - | +0.19 to +0.25 | Most cathodic, noble |
| 36 | Graphite, carbon | - | +0.20 to +0.30 | Most cathodic, noble |
Flowing seawater at roughly 2.4 to 4.0 m/s, 5 to 30 C. Published ranges differ between references by up to 0.05 V; Ag/AgCl seawater values sit within about 0.01 V of SCE.
Metals is listed on the table in order from least cathodic (most anodic) to most cathodic. When you connect two different metals in contact with each other in seawater, the one closer to top of the table will be the anode, the corroding member, while the other, lower in the list, will be the cathode, the protected member.
As you can see, the greater the distance between them in terms of their possible range, the greater will be the driving force for corrosion. Usually, if the couple differs by less than ~0.1 V, the difference is considered insignificant, while values of about 0.2 V or more need design consideration.
Looking at the corrosion potential column, you find the freely corroding potential referenced to a saturated calomel electrode in flowing seawater. Because this varys depending on the water conditions and alloy composition, there’s a range rather than a single number listed in each entry.
Because the two references differ by only about 0.01 V, you can interchange boat-oriented tables from ABYC; they quote just about identical numbers referenced to a silver/silver-chloride electrode. That leaves out the copper/copper-sulfate electrode whose reference is for buried structures, which you don’t want to mix in unless corrected by roughly +0.07 V.
For nickel-chromium alloys and stainless steels, you note the condition column. They is passive and noble in clean water due to their chromium oxide film, but their film breaks down in stagnant water or crevices. This causes the identical grade to drop several hundred millivolts down the series from being noble to active, hence two listings for 304 and 316.
Where crevices are possible, you design pairs to work against the active value, the film breaks down easy in still water.
Three classic traps to look out for: 1) Graphite (including those fancy new carbon-fiber laminated) are on the noble side, meaning they will aggressively corrode steel or aluminum. 2) Copper has a broad enough range that even a moderately sized gap between copper and steel is treated like a real danger. And 3) Galvanized steel acts like Zinc until the coating wears off, then it starts acting more like bare steel, which accelerates corrosion, so you factor that into your design.
Then you apply the series to sacrificial anodes. For example, aluminum anode alloys range from about -1.08 to -1.10V and zinc anodes is around -1.01V. Both remain anodic relative to all common hull metals.
Magnesium is the most anodic material used in the system, but it is only used in freshwater because its driving voltage is higher than what zinc can provides in that medium.
For near neutral, aerated water such as seawater, you take care to apply the table. In hot deaerated systems, acids, or alkalis, the ranking may shift, limiting its use to suitable environments.
You mention that MIL-STD-889D cautions that the galvanic series tells you only which member is the anode; it doesn't tell you how quickly it'll corrode. For that judgment, you should of use the design rules and limits of the anodic index because the series by itself isn't enough to give you the rate of corrosion.
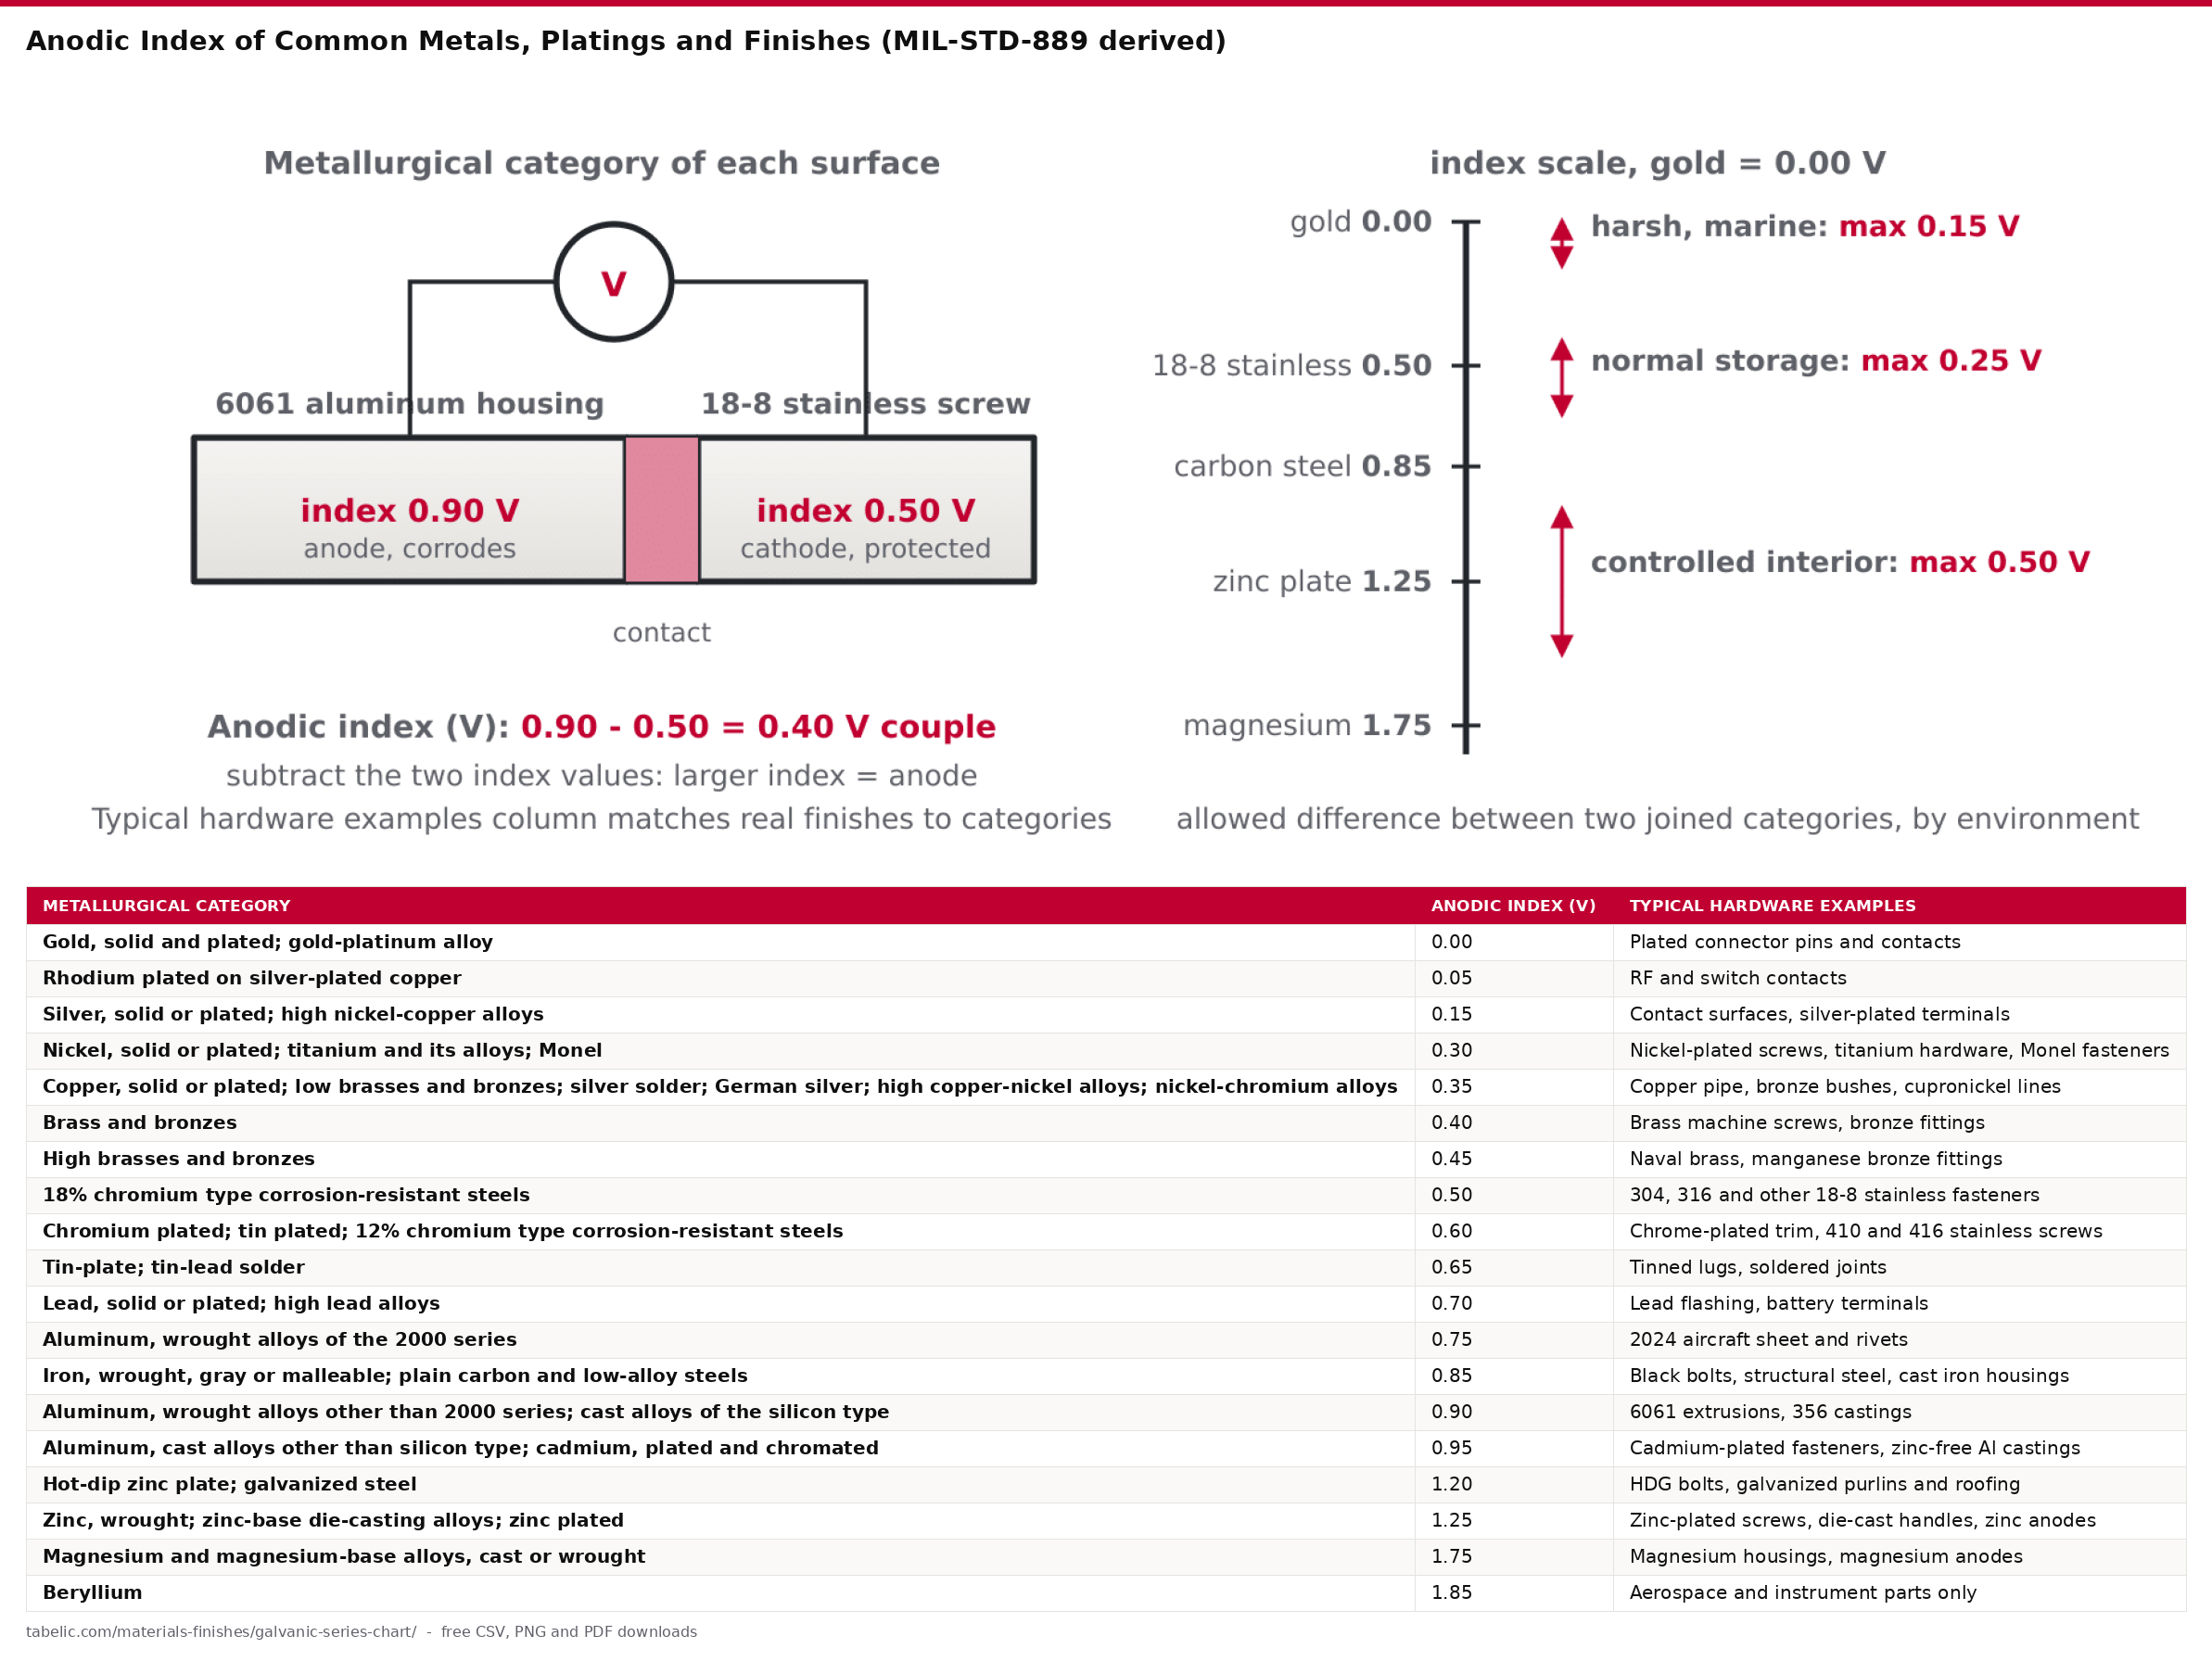
Anodic Index of Common Metals, Platings and Finishes (MIL-STD-889 derived)

| Metallurgical category | Anodic index (V) | Typical hardware examples |
|---|---|---|
| Gold, solid and plated; gold-platinum alloy | 0.00 | Plated connector pins and contacts |
| Rhodium plated on silver-plated copper | 0.05 | RF and switch contacts |
| Silver, solid or plated; high nickel-copper alloys | 0.15 | Contact surfaces, silver-plated terminals |
| Nickel, solid or plated; titanium and its alloys; Monel | 0.30 | Nickel-plated screws, titanium hardware, Monel fasteners |
| Copper, solid or plated; low brasses and bronzes; silver solder; German silver; high copper-nickel alloys; nickel-chromium alloys | 0.35 | Copper pipe, bronze bushes, cupronickel lines |
| Brass and bronzes | 0.40 | Brass machine screws, bronze fittings |
| High brasses and bronzes | 0.45 | Naval brass, manganese bronze fittings |
| 18% chromium type corrosion-resistant steels | 0.50 | 304, 316 and other 18-8 stainless fasteners |
| Chromium plated; tin plated; 12% chromium type corrosion-resistant steels | 0.60 | Chrome-plated trim, 410 and 416 stainless screws |
| Tin-plate; tin-lead solder | 0.65 | Tinned lugs, soldered joints |
| Lead, solid or plated; high lead alloys | 0.70 | Lead flashing, battery terminals |
| Aluminum, wrought alloys of the 2000 series | 0.75 | 2024 aircraft sheet and rivets |
| Iron, wrought, gray or malleable; plain carbon and low-alloy steels | 0.85 | Black bolts, structural steel, cast iron housings |
| Aluminum, wrought alloys other than 2000 series; cast alloys of the silicon type | 0.90 | 6061 extrusions, 356 castings |
| Aluminum, cast alloys other than silicon type; cadmium, plated and chromated | 0.95 | Cadmium-plated fasteners, zinc-free Al castings |
| Hot-dip zinc plate; galvanized steel | 1.20 | HDG bolts, galvanized purlins and roofing |
| Zinc, wrought; zinc-base die-casting alloys; zinc plated | 1.25 | Zinc-plated screws, die-cast handles, zinc anodes |
| Magnesium and magnesium-base alloys, cast or wrought | 1.75 | Magnesium housings, magnesium anodes |
| Beryllium | 1.85 | Aerospace and instrument parts only |
Index values are volts relative to gold at 0.00 V. Subtract two index values to get the galvanic voltage of the couple; the metal with the larger index is the anode and corrodes.
From MIL-STD-889 we gets a fast engineering workaround called anodic index. This gives each metal/finish a single number that indicates its electrochemical voltage relative to gold.
To determine if a pair is good, you simply subtracts one value from another. That’s the voltage potential of the pair. The item with the higher number become the anode, the one that gets eaten away.
Say you have an 18-8 stainless screw (index=0.50). And you’ve got a 6061 aluminum housing (index = 0.90). So what? The difference is 0.40 V. In this scenario, aluminum is anode.
A column group together metals and platings that is similar from an electrochemical standpoint. Remember that a plated piece is considered by what's on top, not underneath. So until it wears through to reveal metal beneath, a zinc-plated steel screw is zinc (index = 1.25). Once it does, it's steel (index = 0.85).
The typical hardware examples column is just for translating purposes. Always refer to the actual finish you're dealing with. For example, a chromated cadmium plate is 0.95, while a tin plate is 0.65 and a zinc plate is 1.25. It is the same steel screw, but it appears in three locations along the scale depending on the finish.
Environment determine what is acceptable. See the table of limitations below.
Harsh: Here you get 0.15 V outdoors, salty, humid environments. Normal: Here you get 0.25 V in storage-type environments. In controlled temperature and humidity, you gets 0.50 V.
In the stainless-on-aluminum example above, the 0.40 V difference fails both the harsh and normal limits. This combination relies on finishing and the small-cathode area rule rather than raw compatibility.
There are two traps to be aware of here: The index reduces all categories down to one number. What it obscures is the active/passive split of stainless steels (see the table of seawater series above). Do not take stainless index arithmetic too serious. Wherever there are stagnant wet conditions or crevices, assume the worst.
The second trap is the sign convention. In some references, these numbers is listed negatively. In those tables, beryllium has a value of -1.85. Gold is -0.00. Only the difference between two entry ever matters. Both conventions yield same answer.
That said, you’re using this table for enclosure design and atmospheric considerations, sheet-metal assemblies, fasteners, brackets, etc. For submerged seawater service, then you’ll be working based off the table of measured seawater series. Immersion amplifies little differences. The index rounds them away.
Allowable Anodic Index Difference by Environment (galvanic compatibility limits)

| Environment class | Typical service conditions | Max anodic index difference (V) | Example pair at the limit |
|---|---|---|---|
| Harsh | Outdoors, high humidity, salt spray, marine and coastal atmospheres | 0.15 | Gold to silver (0.00 vs 0.15); zinc plate to galvanized steel (1.25 vs 1.20) |
| Normal | Warehouse storage, unheated indoor spaces without temperature or humidity control | 0.25 | Carbon steel to tin plate (0.85 vs 0.65); copper to silver (0.35 vs 0.15) |
| Controlled | Temperature and humidity controlled interiors, sealed and conditioned enclosures | 0.50 | 18-8 stainless to aluminum 6061 (0.50 vs 0.90); brass to carbon steel (0.40 vs 0.85) |
Limits per MIL-STD-889 derived compatibility practice. If a required pairing exceeds the limit, interpose plating, insulation or sealing rather than accepting the couple bare.
The table tell you how big a voltage differential you should accept. The anodic index raises this question.
In the first column, you locate where your service environment lie. You subtract the index values for your two metal. Then, in the third column, you see if the values remains equal to or less than the volts listed there. Assuming that they do, you can usually join them together bare. Otherwise, you follow one of the mitigation measure in the final table.
This is the type of electrolyte environment that the joint will actualy experience. Conductive liquid film are required for galvanic corrosion, so the cleaner/drier the environment, the higher voltage it can withstands.
Very conductive film are formed from salt fog and high humidity (like coastal areas). Sea salt has magnesium chloride which begin to absorb water at 34% relative humidity. That is why the limit is so tight on the harsh side, at only 0.15 V.
An interior with controlled air and no condensation can tolerate up to 0.50 V because a continuous electrolyte film is unlikely to form.
Harsh: even indoors in an unconditioned coastal garage; salt-sprayed roadway underbody (salt on the road is bad). Controlled: equipment kept dry within a sealed, conditioned cabinet, even on an oil rig, including enclosed cabinets containing connectors and switches that is protected from weather.
Immersion is beyond even the harsh class; metal permanently under seawater gets designed from the seawater series with insulation and sacrificial anodes, not these atmospheric limits.
By definition, per MIL-STD-889 if you have a necessary combo that’s over the limit, then you don’t scrap the design; instead, you deal with it.
Plating one side towards the other (e.g., zinc or cad plating on steel screws mating to aluminum) is common practice. Interposing a gasket or washer that won’t corrode is another option. And sealing and insulating the joint to prevent a bridge of electrolyte formation is yet another technique.
The mitigation table covers those techniques, row by row.
Fastener and Base Metal Galvanic Compatibility Matrix (atmospheric exposure)

| Base metal (large area) | Carbon steel fastener | Galvanized / zinc-plated fastener | Aluminum fastener | Copper / brass fastener | Stainless steel fastener |
|---|---|---|---|---|---|
| Carbon steel, cast iron | Good (same metal) * | Avoid | Avoid | Good * | Good * |
| Zinc, galvanized steel | Good * | Good (same metal) | Good | Uncertain | Good |
| Aluminum and aluminum alloys | Uncertain to poor | Uncertain | Good (same metal) | Uncertain to poor | Good (best practice) |
| Copper and copper alloys | Avoid | Avoid | Avoid | Good (same metal) | Good |
| Stainless steel (304, 316) | Avoid | Avoid | Avoid | Good | Good (same metal) |
Ratings for outdoor atmospheric exposure per Euro Inox / worldstainless data. * means the couple itself is negligible but the less noble partner rusts on its own and needs its usual protection. Marine spray or immersion is one class more severe: insulate or upgrade.
Find the metal of the part you are fastening in the left column, then read across to the fastener material you plan to use. It’s assuming normal fastening shapes, i.e., that the base metal is large and the fastener is small with respect to wetted areas.
Good indicates the pair is suitable for outdoor practice. Uncertain means it depends on whether dirt, salt, and wetness are kept; the area should of be isolated. Avoid indicates one member or right nearby will be damaged, typicaly either the fastener or the immediate surrounding metal.
One of the physical rules applies to the entire matrix, known as the area ratio effect. It states that corrosion current generated on the cathode will concentrate on the anode.
The worst type of design is having an anodic fastener in a noble structure. For example, a zinc plated screw can be in copper flashing, or an aluminum bolt can be in stainless plate. On the other hand, a small noble fastener in a large anodic structure spreads the attack over such a great area that it's usually tolerable. Standard practice is to use stainless screws in aluminum sheet, even though those two metals is far apart in the series.
The small details of this are marked by starred entries. Galvanic is fine for a stainless screw in carbon steel or a carbon steel bolt in carbon steel. But either one require plating or paint anyway because the steel will rust at its naturaly rate.
On the other hand, don’t forget that if you use a galvanized fastener in a copper or stainless structure, the zinc comes off much faster then when alone. As the zinc-iron alloy layer is approached, the corrosion product shifts from white to orange; beyond that point, the steel core will corrode faster.
Upgrade, don’t gamble: For all coastal and marine structures, use A4/316 stainless fasteners on aluminum rails, masts and fittings with an isolating washer or paste between head and surface. Use silicon bronze fasteners on bronze or copper hardware below the waterline; never use plain or galvanized steel against copper alloys in salt spray.
The Australians give a strong warning for coated roofing. Stainless uninsulated fixings aren't allowed on aluminum zinc-coated sheet because galvanic current cause blisters in the coating at each screw.
For immersion service, seawater is its own deal (sacrificial anodes and the rest of the seawater series), as are magnesium castings, which are not covered in the matrix. Magnesium-compatible coatings can be used on fasteners for magnesium castings; otherwise treat all non-magnesium-compatible fasteners as magnesium risks and segregate accordingy.
Passive stainless and titanium is noble and generally OK as fasteners in most bases, but neither is OK as the base material for anodic fasteners. For immersion service, see sacrificial anodes and the seawater series.
Fastener threads deserve consideration, as well. Any plating is cut through at threads, so specify formed then plated fasteners. Apply anti-seize that’s compatible with the pair to prevent crevice attack in the threaded connection.
Practical Rules to Prevent Galvanic Corrosion (design mitigation checklist)

| Design rule | Why it works | How to apply it |
|---|---|---|
| Make the fastener the noble member | A small cathode in a large anode draws little current per unit area; a small anode in a large cathode is consumed fast | Stainless screws in aluminum or steel sheet are accepted; never aluminum or zinc-plated fasteners in stainless, copper or carbon-fiber parts |
| Keep the anode area about 10x the cathode area | Galvanic current from the cathode spreads across the anode; a large anode keeps current density and metal loss low | Count only wetted surfaces; the 10 to 1 anode to cathode rule of thumb makes galvanic effects minor, and bigger ratios are better |
| Stay under the potential difference limits | A small driving voltage cannot push a damaging galvanic current | Aim under 0.1 to 0.2 V in seawater couples; keep anodic index differences under 0.15 V harsh, 0.25 V normal, 0.50 V controlled |
| Insulate the joint electrically | Breaking the metal-to-metal conduction path opens the circuit, and no galvanic cell can run | Nylon or phenolic washers, shoulder sleeves through the bolt hole, and gaskets on both faces; paint is not reliable insulation under bolt heads |
| Coat the cathode, not just the anode | Shrinking the noble metal's wetted area throttles the whole cell; coating only the anode concentrates attack at every pinhole | Paint the noble member and carry the coating 30 to 50 mm past the joint line; if the anode is coated too, keep that coating defect free |
| Seal and drain the joint | Without a continuous electrolyte film there is no ion path; dry dissimilar metals do not corrode galvanically | Seal faying surfaces and edges, avoid crevices, water traps and dirt poultices, and design for drainage and fast drying |
| Use transition platings and washers | A plating or interposed metal moves the contact surface's effective potential toward the other member | Zinc or cadmium plated steel bolts against aluminum; a compatible metallic washer between incompatible pairs; plate the cathodic member |
| Fit a sacrificial anode | A deliberately most-anodic metal takes the entire couple current and is replaced on schedule | Zinc (MIL-A-18001, about -1.01 V vs SCE) or aluminum anodes in seawater, magnesium in fresh water; bond them electrically and renew when half consumed |
Rules compiled from MIL-STD-889 practice, NPL corrosion guide No. 5, ASSDA FAQ 1 and Euro Inox guidance. Apply them in combination; insulation plus sealing covers most fastened joints.
When one of the above tables indicate that a pair of metals is potentially dangerous but there’s no way around using them in your design, consult this one instead. The rules is listed in approximately the order a designer encounters them: Row 1 to 3 specify the geometry and materials; row 4-6 break the corrosion cell; and row 7 and 8 manage whatever current is left over.
Finally, the why it works column links each rule to one or more of the three necessary conditions for every galvanic cell: two dissimilar conductor, an electrical connection between them, and a common electrolyte. If you eliminate any of these conditions, the corrosion cease.
One rule that gets particular care is the area ratio. In both directions, area ratio overrides the series tables: a terrible-looking pair on paper (say, SS and Al, with 0.40 V apart on the anodic index) is routine if one partner's anode is huge; whereas one that looks mild fail promptly where the anode is tiny.
Caution: after a rain, a wetted-area ratio of 50 to 1 can quickly reduce to 1 to 1 as surfaces dry out unevenly. Judge the worst credible wetting, not the sunny-day case.
Most insulation failures is mechanical. Examples include leaving a sleeve out of one of several hole, re-establishing a conductive path through another piece of cable tray, pipe, or earth strap elsewhere in the assembly, or crushing paint films with a torqued bolt head.
Don’t forget: Anodized aluminum and stainless steel do not use their oxide film as electrical insulation for these purposes. Gaskets made with carbon loading and even graphite is conductors at the high end of the series. They’ve eaten away stainless flange faces in seawater service.
Many folks is surprised by the coat the cathode rule (it goes against your gut, which tells you to shield the stuff that’s getting eaten away). Painting just the anode is risky business. At each pinhole or scratch, all the galvanic current will focus on a few square millimeters of bare anode and drill down deep local pit.
It works better to starve the cell by coating both members or just the more noble one. Because the galvanic interaction occur only a short distance across a thin layer of electrolyte film, make sure the coating extends far past where the two meet; standard advice is 30-50 mm beyond the joint.
The rules address the issue of galvanic corrosion only. This does nothing to eliminate the rate at which any metal corrodes on its own. Even if you have a perfect couple with a carbon steel bracket, that bracket will still rust.
The rules don’t address pitting and other types of corrosion such as stress corrosion cracking or crevice corrosion since those require their own countermeasures. Treat coatings and sacrificial anodes like consumable items and develop an inspection schedule for any structure they’re installed on if it is immersed. It's not a one time thing and you should of checked it.
References
- Galvanic and corrosion compatibility, anodic index and environment limits - Engineers Edge
- Metals in seawater, galvanic series order - The Engineering ToolBox
- Galvanic series of metals in seawater with corrosion potentials (ABYC referenced) - Nordhavn
- Galvanic series chart, potentials vs saturated calomel electrode - Cathwell
- Galvanic series (scale of nobility) with voltage ranges - StructX
- Galvanic series chart, average voltage in saltwater for boat fasteners - Fair Wind Fasteners
- MIL-STD-889D standard practice for dissimilar metals, full text PDF - Corrdesa
- Stainless steel in contact with other metallic materials (Euro Inox guide) - worldstainless
- Bimetallic (galvanic) corrosion risks with galvanised steel and aluminium - British Stainless Steel Association
- Technical FAQ 1: galvanic and dissimilar metal corrosion rules of thumb - ASSDA
- Bimetallic corrosion, guide to good practice in corrosion control No. 5 - NPL
- Galvanic corrosion and the anodic index - Wikipedia
- Galvanic series in stagnant seawater - Wikipedia
Chart images



These tables are provided for general reference only. Always verify the values against the governing standard, your supplier's documentation or a qualified engineer before relying on them for your industrial use case, especially in safety-critical work.